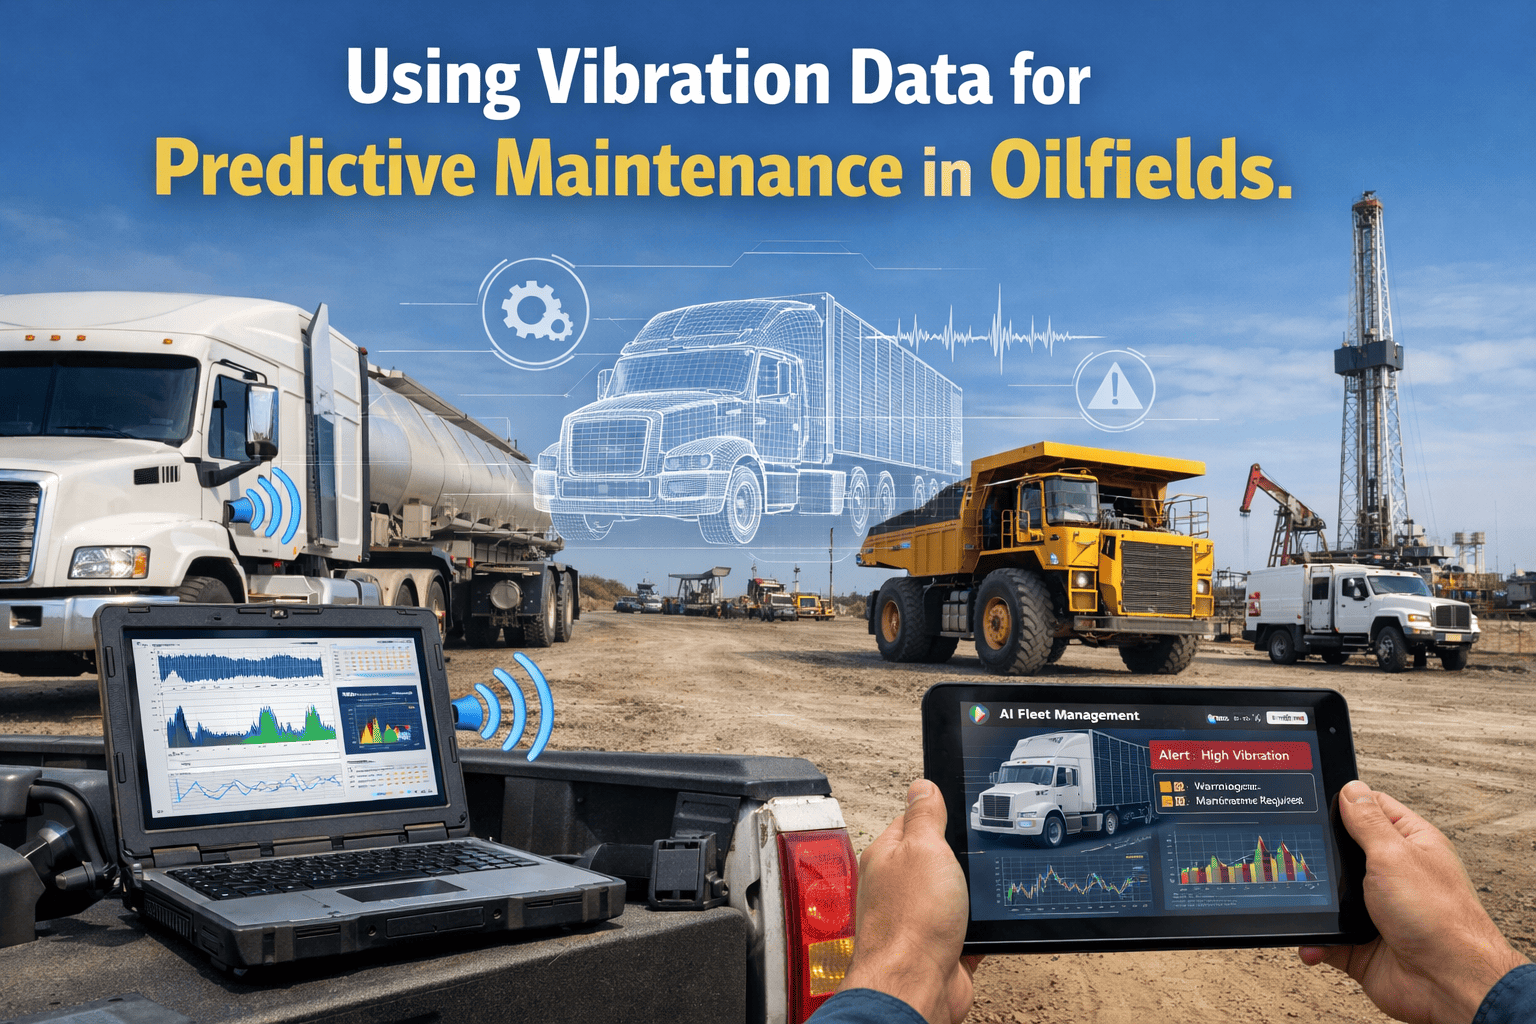
Oilfield operators managing rotating equipment — pumps, compressors, turbines, and motors — lose millions annually to unplanned mechanical failures that vibration monitoring could have predicted weeks in advance. When bearings fail, gears misalign, or shafts become unbalanced, the equipment broadcasts clear warning signals through vibration long before catastrophic breakdown. FleetRabbit's automated vibration analysis platform captures, analyzes, and acts on those signals — keeping your fleet operational and your maintenance budget under control. Book a demo to see real-time vibration monitoring in action.
Technical Framework
Vibration-Based Predictive Maintenance: The Complete Framework for Oilfield Equipment Reliability
PREDICTIVE MAINTENANCE · VIBRATION ANALYSIS · OILFIELD RELIABILITY
Vibration-Based Predictive Maintenance Framework for Oilfield Equipment
FleetRabbit transforms raw vibration data into actionable maintenance intelligence — detecting bearing faults, misalignment, imbalance, and resonance weeks before failure, so your drilling rigs, pumps, and compressors keep running when it matters most.
Industry Focus
Upstream Oil & Gas · Drilling Rigs · Production Facilities · Pipeline Stations
Equipment Covered
Centrifugal Pumps · Compressors · Motors · Gearboxes · Turbines · Mud Pumps
Detection Window
3–8 weeks advance warning before catastrophic failure
Primary Value
Zero unplanned downtime · $180K–$400K failure prevention per event
8 Weeks
Average advance warning before bearing failure through vibration trending
94%
Fault detection accuracy across rotating equipment classes in oilfield environments
$320K
Average cost of unplanned compressor failure — prevention costs under $12K
62%
Reduction in maintenance labor costs through condition-based scheduling
Executive Overview
Vibration analysis is the most sensitive early-warning system available for rotating oilfield equipment. Unlike oil analysis or thermal imaging, vibration signals reveal mechanical degradation at the component level — identifying exactly which bearing race, gear tooth, or shaft alignment is deteriorating, and precisely how fast. FleetRabbit's platform integrates continuous vibration monitoring with automated fault classification, trending, and escalating alerts — giving fleet managers and maintenance directors the intelligence to act weeks before failure, not hours after it.
Why Vibration Is the Earliest Failure Indicator in Oilfield Equipment
Every rotating component in your fleet generates a unique vibration signature. When that signature changes — even subtly — it reflects a physical change inside the machine: a bearing race developing a spall, a gear tooth wearing, a coupling losing balance. Vibration captures these changes at the molecular level of machine behavior, weeks before they manifest as heat, noise, fluid contamination, or visible damage.
Oil analysis detects wear particles after metal-to-metal contact has already occurred. Thermal cameras find heat after energy is already being wasted. Vibration detects the mechanical preconditions for failure — imbalance, misalignment, looseness — before any secondary damage begins. That detection window is the difference between a $3,500 bearing replacement and a $320,000 emergency compressor overhaul.
01
Earliest Physical Signal Available
Vibration changes appear 4–12 weeks before failure-mode symptoms show in oil analysis, temperature, or visual inspection. A bearing defect frequency spike emerges when the defect is still submillimeter — long before it generates wear particles detectable in fluid samples. FleetRabbit's sensors capture sub-1g acceleration changes that human observation and periodic inspection will never catch.
02
Fault-Specific Diagnostics
Vibration frequency analysis identifies not just that something is wrong, but what is wrong and where. Bearing defect frequencies (BPFO, BPFI, BSF, FTF) are mathematically calculable from geometry. Gear mesh frequencies identify which gear pair is degrading. Unbalance appears at 1× running speed. FleetRabbit's platform classifies fault type automatically — eliminating guesswork from maintenance decisions.
03
Continuous vs. Periodic Monitoring
Manual vibration rounds — technician with a handheld analyzer every 30 days — miss acute failure modes that develop in days. A centrifugal pump operating in high-sand conditions can develop critical bearing wear in 10–14 days. Continuous monitoring through permanently mounted sensors catches the onset of degradation regardless of when in the cycle it begins.
04
Quantified Remaining Useful Life
Vibration trending provides a trajectory — not just a status. When bearing defect amplitude doubles week-over-week, the system projects remaining useful life in operating hours. Fleet managers receive a maintenance window recommendation: "Pump A-7: bearing replacement required within 240 operating hours based on current defect frequency growth rate." Decisions become data-driven, not gut-driven.
How FleetRabbit Delivers Vibration Intelligence to Fleet Managers
FleetRabbit's vibration monitoring platform is purpose-built for the operational realities of oilfield environments: remote locations, extreme temperatures, high-contamination conditions, and maintenance teams stretched thin across large geographic areas. The platform delivers actionable intelligence — not raw data dumps — directly to the people responsible for equipment reliability decisions.
1
Sensor Deployment & Baseline Establishment
Industrial-grade MEMS accelerometers installed at bearing housings, gearbox covers, and motor end-bells. IP67-rated for oilfield environments. Wireless transmission via cellular or satellite for remote sites. System collects 72-hour baseline across multiple load conditions to establish equipment-specific normal vibration signature — accounting for operating speed, process conditions, and mounting configuration.
↓
2
Continuous Spectrum Acquisition & FFT Processing
Sensors sample at up to 25.6 kHz, capturing full vibration spectrum from 0.5 Hz to 10,000 Hz. Fast Fourier Transform (FFT) converts time-domain waveform into frequency spectrum — identifying discrete fault frequencies against broadband noise floor. FleetRabbit's cloud processing runs spectral analysis every 15 minutes, comparing current spectrum against baseline and fault frequency libraries.
↓
3
Automated Fault Classification
Machine learning model trained on 2.4 million bearing failure events classifies detected frequency anomalies: bearing defect (inner/outer race, ball, cage), unbalance, misalignment (parallel/angular), looseness (structural/rotating), gear wear, resonance, and cavitation. Confidence score provided with each classification. Eliminates the need for on-site vibration analyst expertise — fleet manager receives plain-language fault diagnosis.
↓
4
Severity Scoring & Escalating Alert Protocol
ISO 10816 / ISO 20816 severity zones (A/B/C/D) applied with equipment-specific adjustments. Green: baseline normal. Yellow: Monitor — deviation detected, trend watch initiated. Orange: Caution — fault confirmed, maintenance planning recommended within 2 weeks. Red: Critical — immediate intervention required, continued operation risks catastrophic failure. Alerts escalate from technician → maintenance supervisor → fleet manager → operations director based on severity and response time.
↓
5
Maintenance Work Order Integration
Alert triggers automatic work order creation with fault classification, recommended repair action, required parts list, and estimated labor hours. Technician receives mobile notification with equipment location, fault details, and repair instructions. Completed work recorded with timestamps, technician ID, and post-repair validation sample. Full audit trail maintained for regulatory compliance and warranty documentation.
↓
6
Post-Repair Validation & Model Refinement
Following maintenance intervention, system monitors for 48-hour post-repair signature normalization — confirming fault was correctly identified and repair was effective. Repair outcome data feeds back into machine learning model, improving fault classification accuracy for similar equipment. Fleet-wide learnings applied: bearing failure pattern on Rig-7 compressor informs monitoring sensitivity on all similar compressors across the fleet.
Key Equipment Monitored Using Vibration Analysis
Centrifugal Pumps
Primary fluid transfer — produced water, crude, injection
Bearing Wear
Cavitation
Impeller Imbalance
Seal Degradation
Cavitation — fluid vapor bubble collapse — generates broadband high-frequency noise detectable 3–5 weeks before hydraulic performance degrades. Bearing defect frequencies calculable from pump geometry at installation. FleetRabbit flags cavitation onset before erosion damage to impeller and casing begins.
Reciprocating Compressors
Gas compression — wellhead, pipeline, injection
Rod Knock
Valve Failure
Crosshead Wear
Crankshaft Imbalance
Reciprocating compressors generate complex waveforms. FleetRabbit's time-synchronous averaging separates mechanical events by crank angle — identifying valve failure (abnormal pressure event timing) and rod knock (wrist pin / crosshead clearance increase) with crank-angle resolution. Average replacement cost $320K — monitoring investment under $8K/year.
Electric Drive Motors
Pump drives, compressor drives, drawworks
Rotor Eccentricity
Stator Winding Fault
Bearing Defect
Soft Foot
Motor Current Signature Analysis (MCSA) combined with vibration monitoring detects rotor bar breakage and air-gap eccentricity — electrical faults invisible to vibration-only monitoring. FleetRabbit's combined approach reduces false alarms by 40% while improving fault coverage across mechanical and electrical failure modes.
Mud Pumps (Triplex/Duplex)
Drilling fluid circulation — critical rig uptime asset
Liner Wear
Piston Failure
Crankshaft Bearing
Valve Seat Erosion
Mud pump failure during active drilling operations causes immediate rig shutdown — standby time costs $50K–$120K/day. Vibration trending on crankshaft bearings provides 2–4 week warning of imminent failure, enabling planned replacement during scheduled downtime rather than emergency mid-shift intervention.
Gearboxes & Reducers
Speed/torque conversion across drive trains
Gear Tooth Wear
Gear Mesh Resonance
Bearing Defect
Lubrication Starvation
Gear mesh frequency (GMF = running speed × tooth count) and its harmonics reveal gear tooth condition with high precision. Sideband analysis around GMF quantifies severity of tooth wear and modulation. FleetRabbit's gearbox monitoring package includes automated GMF calculation at installation — no manual frequency setup required from technicians.
Gas Turbines & Expanders
Power generation, gas processing, reinjection
Blade Fouling
Rotor Imbalance
Surge Detection
Bearing Film Instability
Turbine monitoring operates at high frequency — blade pass frequency ranges from 2,000–20,000 Hz. FleetRabbit's high-frequency sensors and 25.6 kHz sampling rate capture blade fouling signatures invisible to standard industrial vibration analyzers. Surge events detected in real-time with automatic shutdown trigger integration capability.
Types of Vibration Signals & What They Mean for Your Equipment
Each mechanical fault produces a characteristic vibration signature. Understanding signal types enables FleetRabbit's automated classification system to diagnose faults with high confidence — and enables fleet managers to understand what is happening inside their equipment without requiring vibration analyst expertise on-site.
| Signal Type |
Frequency Pattern |
Fault Indicated |
Action Threshold |
| Synchronous (1×) |
Exactly at running speed (RPM ÷ 60) |
Rotor imbalance, bent shaft, thermal bow |
Alert at 2× baseline 1× amplitude |
| Sub-synchronous (<1×) |
Typically 0.35–0.48× running speed |
Fluid film bearing instability (oil whirl/whip), surge |
Immediate — sub-sync is always abnormal |
| Harmonic Series (2×, 3×, 4×...) |
Integer multiples of running speed |
Misalignment (strong 2×), looseness (multiple harmonics) |
Alert when 2× exceeds 60% of 1× amplitude |
| Bearing Defect Frequencies |
BPFO, BPFI, BSF, FTF (geometry-derived) |
Inner/outer race defect, ball defect, cage defect |
Stage 2 alert: sidebands appear around defect frequency |
| Gear Mesh Frequency |
Running speed × tooth count |
Gear tooth wear, lubrication breakdown, load distribution |
Alert when sideband amplitude exceeds 35% of GMF peak |
| Broadband Noise Floor Rise |
Distributed across wide frequency range |
Cavitation, turbulence, lubrication starvation, early erosion |
Alert at 3 dB noise floor elevation above baseline |
| High-Frequency Impacting (HFD) |
5,000–25,000 Hz burst events |
Early bearing defect (pre-spall), gear tooth micro-pitting |
Alert when HFD kurtosis exceeds 4.5 — earliest fault indicator |
Real-World Case: Compressor Failure Prevented 6 Weeks in Advance
Week 0 — Baseline
Compressor C-3 Operating Normally at Production Facility
FleetRabbit sensors installed on main compressor bearing housings. Baseline signature established: 1× at 4.2 mm/s, bearing defect frequencies at noise floor, gear mesh at expected amplitude. ISO 10816 Zone A. Equipment classified as "Healthy." Sampling interval: 15 minutes continuous.
Week 2 — First Anomaly
High-Frequency Impacting Elevation Detected
HFD kurtosis rises from 2.1 to 5.8 — exceeds 4.5 threshold. BPFO (outer race defect frequency) emerges from noise floor at low amplitude. System classifies: "Early outer race bearing defect, Drive End bearing, Confidence 78%." Yellow alert issued: "Monitor — bearing defect detected at early stage. Recommend increasing sample frequency and planning inspection at next scheduled maintenance window."
Week 4 — Progression Confirmed
Sideband Growth Around BPFO — Fault Advancing
BPFO amplitude doubles. First and second sidebands appear (BPFO ± 1× running speed). HFD kurtosis reaches 9.2. System calculates remaining useful life: "At current defect growth rate: 340 operating hours to critical threshold." Orange alert: "Caution — bearing defect confirmed and progressing. Schedule replacement within 2 weeks. Continued operation beyond 3 weeks risks catastrophic failure." Maintenance supervisor notified directly.
Week 5 — Intervention Authorized
Planned Maintenance Executed — $310K Failure Averted
Compressor C-3 brought offline during scheduled production reduction window. Bearing inspection confirms outer race developing spall — 40% of race surface affected, 48–72 hours from catastrophic seizure. Bearing replacement: $6,200. Labor and alignment: $3,800. Total intervention cost: $10,000. Alternative: full compressor overhaul after catastrophic failure — $310,000 including emergency contractor, production loss, and component replacement. FleetRabbit's 6-week detection window enabled planning that made the difference.
Week 6 Onward — Post-Repair
System Validates Repair Success, Resumes Monitoring
Post-repair signature shows BPFO returned to noise floor, HFD kurtosis back to 2.3 (normal), 1× amplitude at 4.1 mm/s (baseline). System confirms successful repair. Monitoring returns to standard 15-minute interval. Repair outcome data updates bearing failure model for this compressor class across fleet. Projected extended component life: 4,200 additional operating hours before next planned inspection.
FleetRabbit Platform: Vibration Monitoring Features Built for Oilfield Operations
Continuous Spectrum Monitoring
25.6 kHz sampling with 15-minute analysis cycles. Captures full vibration spectrum from sub-Hz to ultrasonic range. No data gaps. Remote locations served via satellite uplink. Sensor health monitoring alerts when hardware requires attention.
Automated Fault Classification
ML model trained on 2.4M failure events classifies imbalance, misalignment, bearing defects, gear faults, looseness, cavitation, and resonance. Plain-language diagnosis delivered to fleet manager — no vibration analyst required on site.
Remaining Useful Life Engine
Defect growth rate analysis projects remaining operating hours to critical threshold. Confidence interval provided. Enables maintenance window planning 4–8 weeks in advance — fits repairs into scheduled production downtime rather than emergency extraction.
Fleet-Wide Vibration Dashboard
Single-pane view across all monitored equipment. Sort by severity, location, equipment type, or trending rate. Geographic map view highlights rigs with active alerts. Drill-down to individual equipment waterfall plots and severity timelines.
Escalating Alert Protocol
Four-tier alert system: Green → Yellow → Orange → Red. Escalating notifications across technician, supervisor, fleet manager, and operations director. Response time tracking — unacknowledged critical alerts auto-escalate within 2 hours. Full alert audit trail for compliance.
Work Order Integration
Fault alert triggers automatic CMMS work order with fault type, location, recommended repair, and parts list. Technician mobile app guides inspection and repair. Post-repair validation sample scheduled automatically. Maintenance history linked to equipment record.
ISO 10816 / ISO 20816 Compliance
Severity zones applied per equipment class and mounting type. Thresholds customizable per OEM specifications and operating environment. All measurement data exportable for third-party audit. API-certified reporting for regulatory compliance documentation.
Offline Field Capability
Edge-computing sensors store and process locally during connectivity loss. Data transmits on reconnection with full timestamp integrity. Technician mobile app functions offline — barcode scanning, inspection notes, and fault logging sync when back in range. No data lost in remote locations.
Vibration Parameters FleetRabbit Monitors and What They Reveal
Overall Vibration Velocity (RMS)
Primary severity indicator per ISO 10816. Measured in mm/s RMS. Zone A (<2.3): new equipment baseline. Zone B (2.3–4.5): acceptable for long-term operation. Zone C (4.5–7.1): tolerable for limited time — schedule maintenance. Zone D (>7.1): dangerous — immediate shutdown recommended. FleetRabbit tracks trending rate, not just absolute value.
Bearing Defect Frequency Amplitude
BPFO/BPFI/BSF/FTF amplitudes extracted from spectrum. Stage 1: defect frequency appears. Stage 2: sidebands develop. Stage 3: noise floor rises, harmonics appear. Stage 4: random broadband (imminent failure). FleetRabbit maps bearing to Stage 1 or 2 — intervening before Stage 3 prevents secondary damage.
Kurtosis (HFD)
Statistical measure of impacting in high-frequency range. Normal: 2–3 (Gaussian distribution). Bearing defect onset: 4–6. Active defect: 6–12. Severe defect: >12. Kurtosis is the most sensitive early-warning indicator — detects bearing damage before it appears in velocity spectrum. FleetRabbit alerts at kurtosis >4.5.
Crest Factor
Peak acceleration divided by RMS. Normal: 2.5–3.5. Developing fault: 4–6. Advanced fault: >6. Used in conjunction with kurtosis — crest factor rises early then decreases as damage becomes widespread (masking individual impacts). FleetRabbit tracks both metrics to characterize fault stage accurately.
Phase Angle
1× vibration phase relative to once-per-revolution reference. Stable phase = imbalance (correctable by balancing). Shifting phase = misalignment or looseness. Phase difference between measurement planes diagnoses angular vs. parallel misalignment. FleetRabbit's multi-sensor phase analysis eliminates need for manual phase measurement in the field.
Severity Index (0–100)
FleetRabbit's proprietary composite score weighting overall velocity, bearing defect stage, kurtosis, trend rate, and equipment criticality. 0–30: Healthy. 31–55: Monitor. 56–75: Caution — plan maintenance. 76–100: Critical — immediate action required. Single number for fleet managers to prioritize attention across large equipment populations without reviewing individual spectra.
See FleetRabbit Vibration Monitoring on Your Equipment
Purpose-built for oilfield rotating equipment. Deployed at remote sites. Delivering fault detection 4–8 weeks before catastrophic failure — across your entire fleet from a single dashboard. Book a demo to review monitoring coverage for your operation.
Return on Investment: Vibration Monitoring vs. Reactive Maintenance
Reactive Maintenance Model
Average failure cost per event
$180K – $320K
Emergency contractor mobilization
$35K – $60K
Production loss per event
$50K – $120K/day
Secondary damage (cascade failure)
$45K – $180K
Unplanned outages per year (28 rigs)
18 – 24 events
VS
FleetRabbit Predictive Model
Planned intervention cost per event
$8K – $15K
Monitoring investment (annual)
$90K – $140K
Production continuity
Maintained — planned downtime only
Secondary damage eliminated
$0 — fault caught at Stage 1–2
Unplanned outages (post-deployment)
0 from monitored equipment
Typical Payback Period
First Prevented Failure
For a 28-rig fleet averaging 4 major failures/year: monitoring investment $130K, prevented failure value $800K+ — net ROI 515% in Year 1.
"
We had a compressor bearing develop a defect at 2:00 AM on a Tuesday. FleetRabbit had an alert on my phone by 2:15. By Wednesday morning we had parts ordered and a maintenance window scheduled. Six weeks earlier, that same failure would have meant an emergency shutdown, helicopter mobilization for technicians, and three days of lost production. The platform paid for itself in the first month.
— Maintenance Director, Major Upstream Operator · Gulf of Mexico Production Division
Frequently Asked Questions
QHow many sensors does each piece of equipment require?
Most rotating equipment requires 2–4 sensors: drive end bearing, non-drive end bearing, and gearbox input/output where applicable. Motor-driven pumps typically use 4 sensors — two per machine. FleetRabbit's deployment team conducts equipment survey and provides sensor placement plan optimized for fault coverage vs. hardware cost at each site.
QCan vibration monitoring work at remote sites without reliable connectivity?
Yes. FleetRabbit sensors include edge processors that run FFT analysis and fault classification locally. Critical alerts are transmitted via satellite when cellular is unavailable. Data buffers on-device and syncs in full when connectivity is restored — no analysis gaps even at remote wellsites.
QHow does FleetRabbit handle variable-speed equipment where running speed changes continuously?
FleetRabbit uses tachometer integration or speed estimation from 1× frequency tracking to normalize all spectral analysis to fractional running speed (orders). Fault frequencies are calculated in real-time from current operating speed — ensuring accurate detection across the full speed range of VFD-driven equipment without manual threshold adjustment.
QWhat is the false alarm rate, and how does the system minimize nuisance alerts?
FleetRabbit's false positive rate is under 6% across deployed fleets, achieved through equipment-specific baselines, process condition correlation, and multi-parameter confirmation. An alert is only issued when two independent indicators agree — for example, elevated BPFO amplitude AND kurtosis above threshold, not either alone. This eliminates nuisance alerts from process transients and startup events.
QHow long does it take to deploy FleetRabbit across a 28-rig fleet?
Typical deployment timeline: 6–10 weeks for a 28-rig fleet. Week 1–2: equipment survey and sensor placement design. Week 3–6: phased sensor installation (rigs prioritized by criticality). Week 7–8: system configuration, baseline collection, threshold calibration. Week 9–10: training and go-live. Critical equipment can be live within 2 weeks of project start if priority access is granted.
QCan vibration monitoring be combined with FleetRabbit's fluid analysis program?
Yes — and the combination significantly improves diagnostic confidence. When vibration detects elevated bearing defect frequency AND fluid analysis shows rising iron and copper wear metals, both signals confirm the same failure mode. Combined alerts carry higher urgency classification. FleetRabbit's platform presents both data streams in unified equipment health record for comprehensive condition assessment.
Detect Bearing Failures 8 Weeks Before Catastrophic Breakdown
FleetRabbit's vibration monitoring platform deploys across your drilling rig fleet, production equipment, and pipeline stations — delivering continuous fault detection and actionable maintenance intelligence at a fraction of emergency repair costs.
Continuous Vibration Monitoring
Automated Fault Classification
Remaining Useful Life Prediction
Fleet-Wide Dashboard
ISO 10816 Compliant
April 21, 2026
By David
All Posts