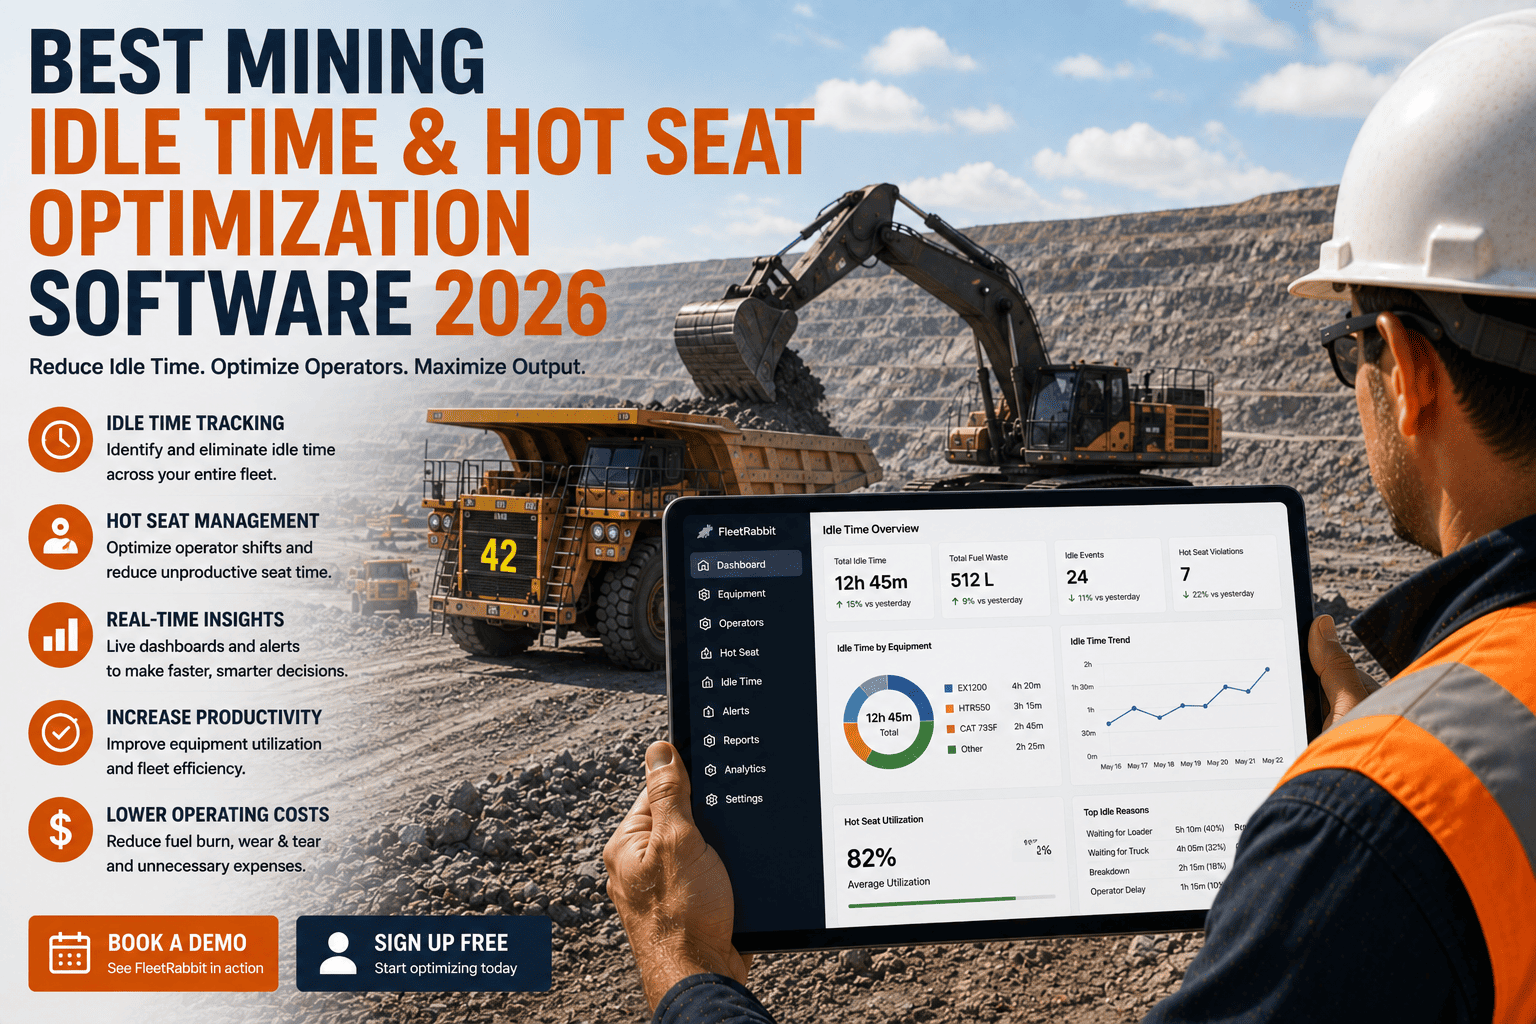
A haul truck parked at the shift change point for twenty minutes while the outgoing operator finishes paperwork and the incoming one grabs coffee looks harmless on any single day. Multiply that gap across every truck, every shift change, every day of the year, and it becomes one of the largest sources of lost production on the entire site, quietly hiding behind a roster that looks fully staffed and a fleet that looks fully scheduled.
Studies of real mining fleets have found shovels running at an average effectiveness of just 25 percent and haul trucks around 38 percent, with poor coordination, not mechanical failure, as the dominant cause. Mines that track idle time automatically and coordinate hot seat changeovers commonly cut operating costs by up to 28 percent within a year by putting that lost capacity back to work.
Where Idle Time Actually Comes From
Idle time rarely comes from one obvious cause. It builds up from a handful of small, repeated gaps that individually look insignificant but compound into a major production shortfall once you add them across a full fleet and a full year.
Dispatch And Queueing Delays
A haul truck waiting on a loader, or a loader waiting on the next truck in line, spends real time not moving material even though the engine is running and the shift clock is ticking. Coordinated dispatch shrinks these gaps by matching equipment availability to the actual pace of the pit.
Uncoordinated Hot Seat Changeovers
A hot seat changeover, where one operator steps out and another steps in without shutting the machine down, is meant to keep equipment running through shift changes and meal breaks. Done without coordination, it produces the opposite result, with machines parked and idling while the incoming operator is still walking across the yard.
Why Poor Hot Seating Is Also A Safety Issue
Rushed, uncoordinated changeovers do not just waste time, they also create real safety risk, since an incoming operator moving into position around an idling machine is exactly the scenario behind several serious mine site incidents. A well-run hot seat process protects both production and people at the same time.
Lack Of Real-Time Visibility
Without live tracking, a supervisor sees a shift roster and a truck count, not the actual minute-by-minute status of every asset. Idle patterns that repeat every single shift stay invisible until someone finally reviews the numbers weeks or months later.
| Changeover Approach | What Happens At Shift Change | Typical Idle Minutes | Visibility Into The Pattern |
|---|---|---|---|
| Uncoordinated Changeover | Machine parks and waits while the next operator finishes briefing and walks over | 10 to 20 minutes per changeover, per machine | None, treated as a normal part of the shift |
| Manually Scheduled Hot Seating | Relief operators are pre-assigned, but timing still relies on radio coordination | 5 to 10 minutes per changeover, per machine | Partial, dependent on supervisor notes |
| Software-Optimized Hot Seating | Live location and status data times relief operator arrival to the machine directly | Under 3 minutes per changeover, per machine | Full, tracked automatically across every asset and shift |
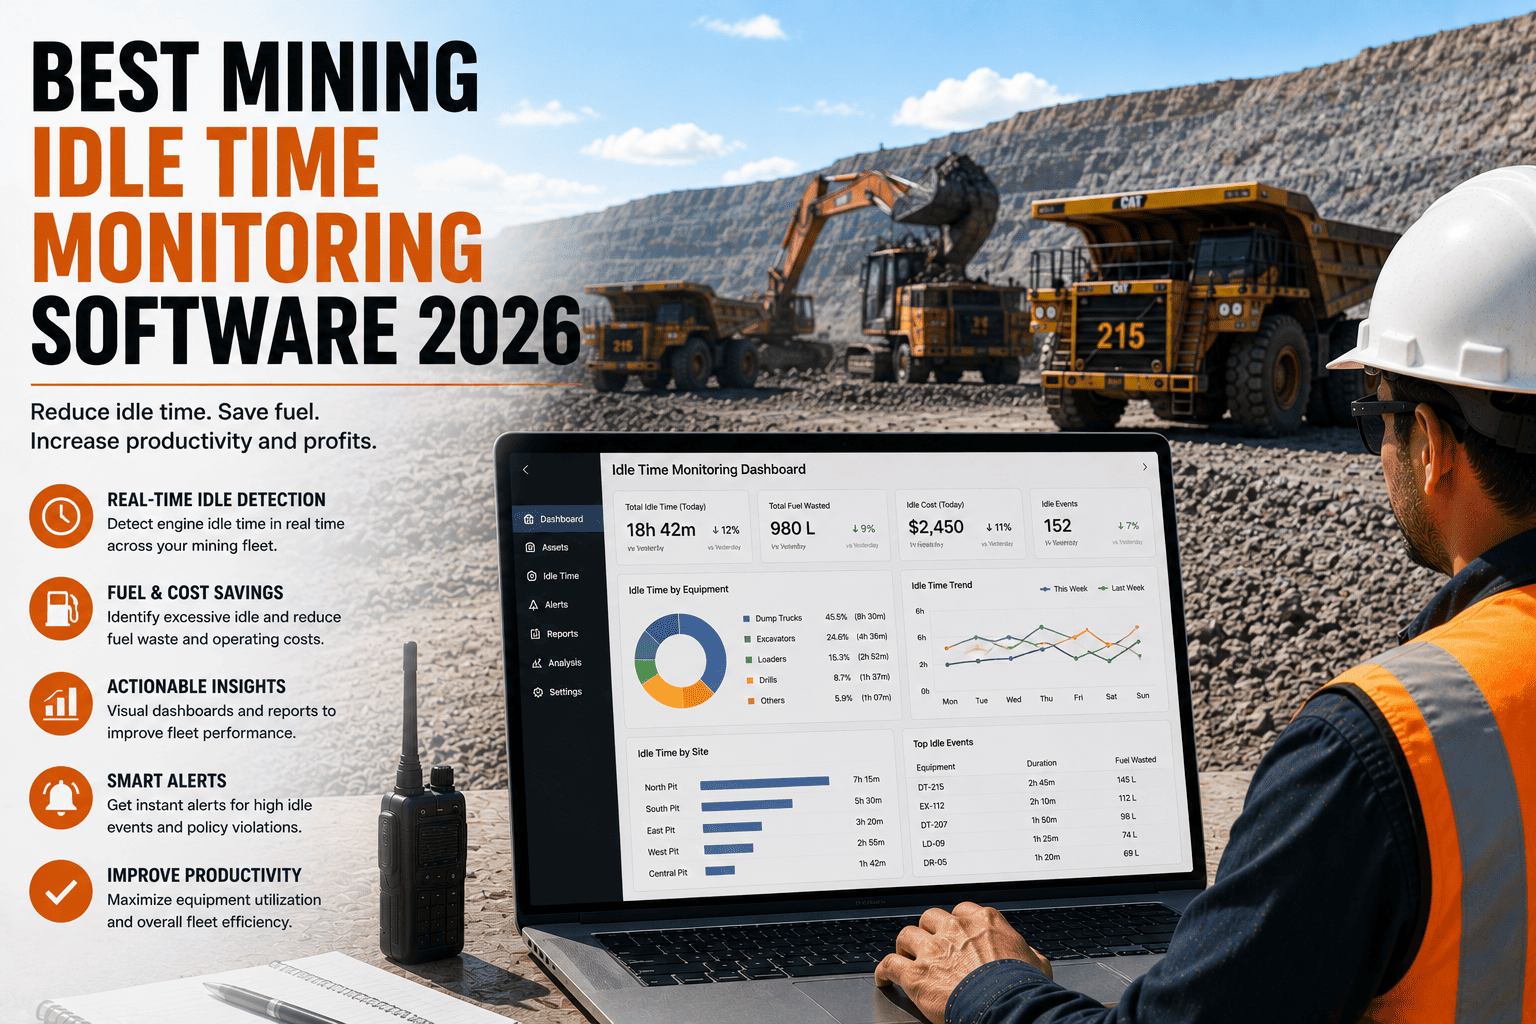
FleetRabbit tracks real-time idle time, dispatch delays, and hot seat changeover duration across every haul truck, loader, and excavator on site, automatically. Operations leaders ready to see exactly where production hours are disappearing can start a free trial today.
Building A Hot Seat Optimization Program
Fixing idle time is not about pushing operators to work faster, it is about closing the coordination gaps that force a perfectly good machine to sit parked between shifts. A structured optimization program tackles this in stages rather than trying to fix everything at once.
Step One: Establish A True Utilization Baseline
Before changing anything, measure actual productive hours against scheduled hours for every asset class. Many operations are surprised to find utilization sitting closer to 55 to 70 percent rather than the 80 to 85 percent achieved by best-in-class sites.
Step Two: Time Relief Operator Arrival To Machine Location
Rather than scheduling changeovers by clock time alone, use live location data to route the incoming operator to arrive exactly when the outgoing operator is ready to step out, cutting the parked, waiting window down to seconds instead of minutes.
Step Three: Flag Idle Patterns As They Happen
Automatic idle-time alerts catch a machine sitting still longer than expected in the moment, rather than surfacing the pattern in a report weeks later when the production hours are already gone.
Step Four: Review Fleet-Wide Trends Weekly
A short weekly review comparing idle time and changeover duration across every asset and shift keeps the improvement compounding instead of fading once the initial rollout excitement wears off.
Metrics That Prove Your Idle Time Program Is Working
Operations leaders who want to see exactly how these numbers look across their own fleet can book a personalized demo and walk through a live utilization dashboard.
Frequently Asked Questions
Idle time and slow hot seat changeovers hide inside a schedule that looks fully staffed and a fleet that looks fully utilized. FleetRabbit exposes every idle minute across every asset, and helps you time hot seat changeovers down to seconds instead of minutes. Start free and see exactly how much production time is waiting to be recovered.