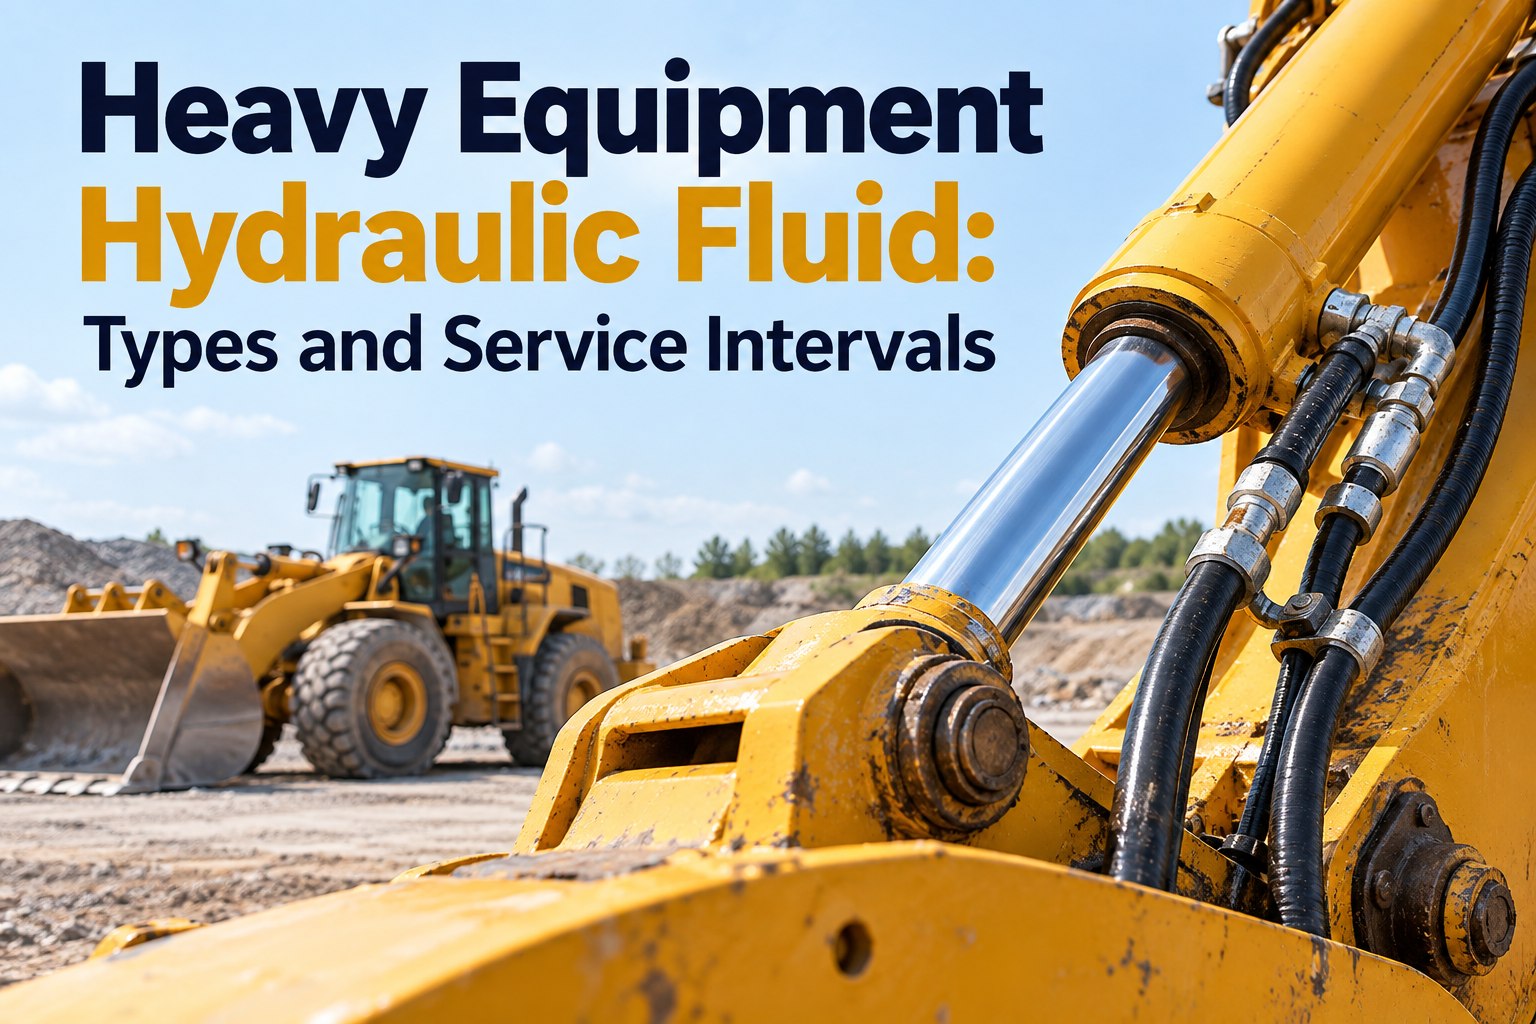
Hydraulic fluid is not a consumable that gets topped up and replaced on a calendar — it is the component that carries the power, lubricates the pump, removes the heat, seals the clearances and transports every particle the machine generates. Two numbers govern whether it does that job: the ISO viscosity grade, which is simply the fluid's kinematic viscosity in centistokes at 40°C, and the ISO 4406 cleanliness code, three numbers counting particles at 4, 6 and 14 micrometres per millilitre. Contamination is the leading cause of premature hydraulic component failure, and water is the part most fleets never measure — mineral oil saturates at roughly 100 ppm at 70°F, and Cantley's bearing research found life extended by a factor of five at 25 ppm dissolved water against 400 ppm near saturation. This guide covers what the fluid does, where contamination enters, how to read both codes, how to choose a grade, the symptoms that name the fault, and what the service interval should actually be. Book a 30-minute demo to see fluid samples and changes tracked per machine, or start free with 3 vehicles.
The Oil Is Not the Consumable. The Filter Is. The Oil Is a Component You Can Test.
For fleet mechanics, shop leads and maintenance managers: how to read an ISO cleanliness code, choose a viscosity grade, control water, and set a service interval on evidence instead of a calendar.
No credit card required. Works alongside your existing oil analysis programme.
What Hydraulic Fluid Is Actually Doing in the Machine
Five jobs at once, and a fluid that fails at any one of them produces a symptom people usually blame on a pump or a valve. Knowing which job has failed is most of the diagnosis. Keep fluid findings on each machine's record with a free account.
- Carries pump output to every cylinder and motor
- Nearly incompressible, so movement is immediate
- Loses efficiency the moment air is entrained
- Any leak is lost work, not just lost oil
- Separates pump, motor and valve surfaces
- Film thickness depends on viscosity at temperature
- Too thin and metal touches metal
- Too thick and the pump cavitates on start-up
- Moves heat from the work back to tank and cooler
- Fluid temperature decides how long the oil lasts
- A failed cooler shortens oil life before it stops the machine
- Tank level affects how much heat can be shed
- Fills gaps inside pumps and valves measured in microns
- Thinning oil lets internal leakage rise
- Slow, weak function is often a viscosity problem
- Worn clearances need the specified grade, not a thicker one
- Moves particles and water toward the filters
- Which is why the filter, not the oil, is the consumable
- Additives suspend what they can until they deplete
- Sampling the oil is how you read the whole system
Airborne dust and humid air enter through the breather every time the level moves. A poor or missing breather element contaminates a whole system quietly.
A restricted or aerated inlet is the fastest way to destroy a pump. Suction-side strainers, low level and a loose fitting all show up here first.
Spool clearances are measured in microns, which is why the particle sizes in the cleanliness code are set where they are.
Every retraction draws the exposed rod back into the seal. A scored rod or a failed wiper pulls outside dirt directly into the circuit.
The last chance to catch what the machine generated before it reaches the tank and gets pumped round again.
Heat control is oil life. A blocked cooler core or a failed fan ages the fluid long before it disables the machine.
Schematic is simplified to show the six points that matter for fluid condition. Real circuits add accumulators, pilot lines and case drains, each of which is another route for dirt and another place to sample.
How to Read an ISO 4406 Cleanliness Code
The code is three numbers, and each one counts particles above a size in one millilitre of fluid. The scale is logarithmic — every step up roughly doubles the particle range — so a code that looks one number worse is twice as dirty. We'll set cleanliness targets per machine class in a demo.
The silt-sized majority. Invisible, and what wears clearances over months.
The band most filter ratings are quoted against.
Big enough to jam a spool or score a swash plate outright.
Particle counts per ISO 4406 as published by Donaldson Hy-Pro. Each increase of one code number represents roughly double the number of particles in that range.
| Component | Typical target | Why |
|---|---|---|
| Servo valves | 16/14/11 or lower | The tightest clearances in the system set the target for everything sharing the tank |
| Proportional and high-pressure valves | Cleaner than general circuits | Follow the component maker's figure, not a fleet-wide default |
| Piston pumps and motors | Mid-range targets | Sensitive to both particles and water; they usually fail before the valves do |
| General mobile circuits | Looser targets acceptable | Still worth measuring — the number only means something once you trend it |
Servo valve target per Donaldson Hy-Pro guidance on ISO 4406 cleanliness codes. Other rows describe the principle rather than a published figure — take the actual target from each component maker, and remember the most sensitive component sharing the tank sets the number for the whole system.
Can You Produce the Last Three Oil Samples for Any Machine in Your Yard?
Most fleets have the reports somewhere and the trend nowhere. In 30 minutes we'll load your sample history against the machines it came from, show which units are drifting between services, and set the change interval on evidence rather than on hours alone.
Water in Hydraulic Oil: The Contaminant Nobody Measures
Water appears in three states depending on how much the fluid is holding, and the damage starts in the state you cannot see. Mineral oil saturates at around 100 ppm at 70°F while ester-based fluids hold more than 3,000 ppm at the same temperature, so "clear oil" proves nothing without a number. Record water content with every sample, free on 3 vehicles. Swipe the table on mobile.
| State | What you see | What it is doing |
|---|---|---|
| Dissolved | Held in solution, invisible — the oil still looks clear | Already causing harm: Cantley's work showed bearing life extended fivefold at 25 ppm versus 400 ppm near saturation |
| Emulsified | Past saturation, suspended as droplets — the milky or hazy look | Film strength and load capacity drop; oxidation accelerates |
| Free | Separated out, usually lying in the bottom of the tank | Corrosion, and in ester fluids hydrolysis that produces acids |
Keep water at 50% of saturation or less
That keeps free water from forming and slows the reactions that need moisture. Two consequences follow: saturation falls as temperature falls, so a fluid that is fine at operating temperature can drop free water overnight during a shutdown — and dissolved water alone, long before anything looks milky, is enough to drive metal fatigue and cut bearing life several times over.
Saturation figures, the three states, the 50% target and the Cantley (1977) bearing-life finding are reported by Machinery Lubrication in its coverage of water contamination in hydraulic and lube systems.
Choosing a Viscosity Grade for the Temperature It Will Actually Run At
An ISO viscosity grade is the fluid's kinematic viscosity in centistokes at 40°C — ISO VG 46 is 46 cSt at 40°C, and so on. What matters in service is that viscosity falls steeply as the oil heats, so the grade has to keep the fluid inside the maker's window at both ends of the working day, not just at the test temperature. We'll review your grades against duty cycle in a demo.
Curves are indicative and drawn to show shape and separation, not measured values for a specific oil. The grade numbers are definitional: an ISO VG grade is the fluid's viscosity in centistokes at 40°C. Take the operating window from the pump and valve manufacturers.
The pump usually has the narrowest viscosity window in the system, and it is the most expensive thing on the circuit.
A machine working hard in summer spends its life at the thin end of the curve, where film strength and internal leakage are decided.
Oil too thick at start-up starves the pump inlet. A cold-climate fleet often needs a different grade, not a longer warm-up.
Going up a grade to mask internal leakage raises operating temperature and ages the oil faster, which accelerates what it was meant to hide.
What the Fluid Is Telling You: Symptoms and Their Real Causes
Hydraulic complaints arrive as behaviour — slow, noisy, hot, leaking — and nearly all of them trace back to viscosity, contamination, water, air or heat. Read the symptom against the cause before ordering a pump. Log symptom, sample result and repair together, free. Swipe the table on mobile.
| What the operator reports | Usual cause | What to do first |
|---|---|---|
| Slow or weak operation when hot | Viscosity too low at operating temperature, or internal leakage past worn clearances | Check oil temperature and grade before condemning the pump |
| Noisy pump, especially on start-up | Aeration or cavitation — inlet restriction, low level, or oil too thick when cold | Inspect the suction side and check cold-start viscosity |
| Milky or hazy oil | Water past the saturation point and emulsified | Sample it — appearance confirms nothing on its own |
| Dark oil with a burnt smell | Thermal degradation and oxidation, usually a heat problem | Find the heat source; new oil will do the same thing |
| Foam on the tank surface | Air entrainment from a leak on the suction side or a low level | Look for the air path, not an additive fix |
| Filters blocking early | The system is generating debris, or the oil arrived dirty | Cut the filter open and identify what it caught |
| Seals failing repeatedly | Heat, contamination or the wrong fluid for the seal material | Confirm fluid compatibility before fitting more seals |
Setting a Service Interval on Evidence Instead of a Calendar
A fixed hour interval either changes good oil or leaves bad oil in the machine, and you cannot tell which without sampling. The programme below replaces the guess, and it fits inside an existing preventive maintenance schedule. See sampling scheduled automatically in a demo.
Level at the sight glass, visible leaks, oil temperature against normal, and any new noise from the pump. Report it on the inspection report rather than mentioning it.
A live, turbulent point in the circuit, same location and same method every time, so results compare. A sample from the tank bottom tells you about the tank bottom.
Particle count against your target, water content against saturation, and viscosity against the grade you believe is in there.
A sample that has moved is worth more than a sample that is merely acceptable. Rising particle counts between services mean the system is generating debris.
Changing the oil without finding out why it failed
New fluid in a system with a blocked cooler, a failed breather or a scored rod will arrive at the same condition on the same schedule. The sample is the diagnosis; the change is only the repair. Record the cause alongside the change or the next report will read the same.
What Hydraulic Fluid Problems Cost, Caught Early Versus Caught Late
The fluid itself is the cheapest item on this list, and a pump is not. Industry benchmarking puts unplanned downtime at roughly $448 to $760 per truck per day before towing and repair, and ATRI puts 2025 repair and maintenance cost at $0.215 per mile, up 8.6% — a useful frame for machines that earn only while they are moving. Track your own hydraulic spend per machine free.
Relative cost by where the problem is caught, illustrative — not prices. Downtime benchmark: FleetNet America and ATA's Technology & Maintenance Council via industry reporting; per-mile cost: ATRI.
Hydraulic Fluid Questions Fleet Mechanics Ask
What does an ISO 4406 code like 19/17/14 mean?
Three particle counts per millilitre of fluid: particles at or above 4, 6 and 14 micrometres. A 19/17/14 code means roughly 2,500 to 5,000 particles at 4 µm, 640 to 1,300 at 6 µm and 80 to 160 at 14 µm. Each step up the scale roughly doubles the range. See targets set per machine.
What ISO viscosity grade should I use?
The grade is the fluid's viscosity in centistokes at 40°C, so ISO VG 46 is 46 cSt at 40°C. Pick the grade that keeps the oil inside the pump and valve maker's window at your actual hot operating temperature, then confirm it is not too thick for a cold start. Record grades per machine free.
How much water is too much in hydraulic oil?
Aim to keep water at 50% of saturation or less. Mineral oil saturates at about 100 ppm at 70°F, so the numbers are small — and dissolved water damages bearings long before the oil looks milky. Review your water results with us.
Why is my hydraulic oil milky?
Water past the saturation point, emulsified through the fluid. It confirms there is a water ingress route — a breather, a cooler, a seal or storage — and the route matters more than the oil change. Log the ingress cause with the change, free.
How often should hydraulic fluid be changed?
On condition rather than on the calendar wherever sampling is practical. Sample from the same live point each service, read particle count, water and viscosity, and change when the trend moves — not when a number is merely acceptable. Set the sampling schedule with our team.
Can I mix hydraulic fluids?
Treat it as a last resort. Different base stocks and additive packages are not guaranteed compatible, and ester-based fluids in particular behave differently with water and with seal materials. Confirm with the fluid supplier before topping up with anything other than the specified product. Record what went in, free on 3 vehicles.
Every Sample, Every Change, Every Cause — On the Machine That Produced It
FleetRabbit holds oil sample results, fluid changes, filter and breather service and the cause behind each one against the machine, so a repeat result reads as a pattern rather than a purchase — and every operator report becomes a work order with that history attached.
No credit card required. Start with your next sample.