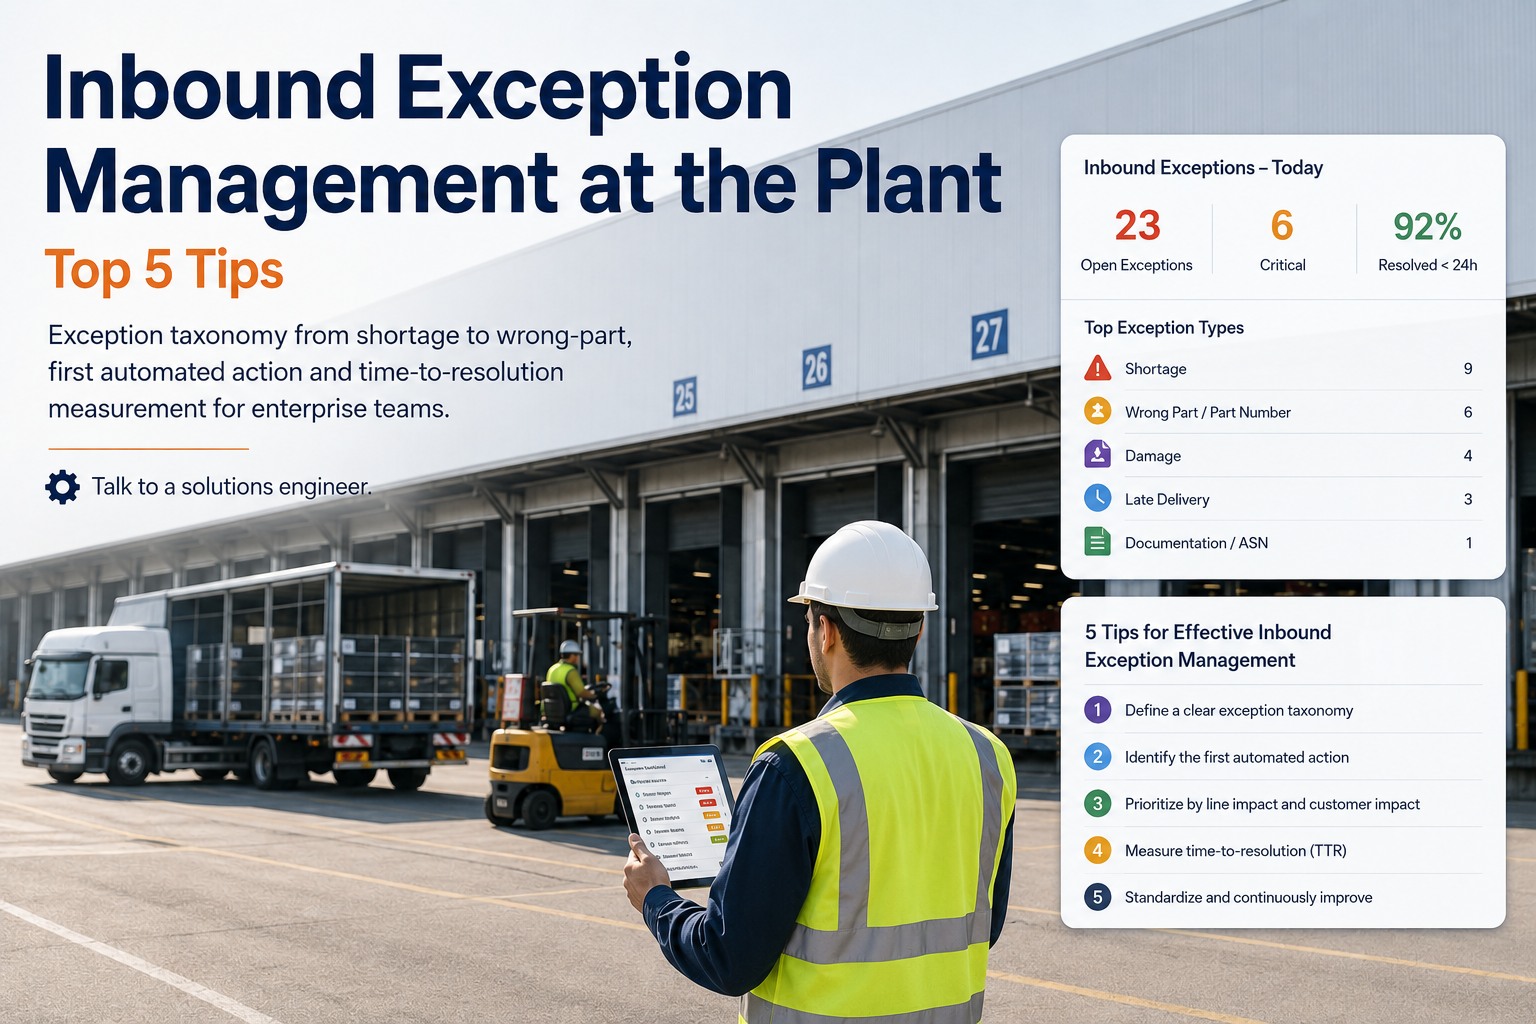
Every plant has an exception process. Very few have one that runs faster than the problem does. The usual shape is a discovery at the dock face, a phone call, a WhatsApp photo, a supervisor walking over, and somewhere between forty minutes and two shifts later a decision — by which point the trailer has either been sent away with material the line needed or received into stock with material it cannot use. Neither outcome is a system failure; both are the predictable result of a process where the first action is human. In a plant feeding a sequence window, the first action has to be automatic, because the expensive part of an exception is almost never the resolution itself — it is the interval between discovery and the first containing step, during which nobody downstream knows anything is wrong. What follows is a working taxonomy, the five things that most reduce that interval, and how to measure time-to-resolution in a way that survives scrutiny. Talk to a solutions engineer to map it against your own receiving flow.
TOP 5 · INBOUND EXCEPTIONS
Inbound Exception Management at the Plant
A taxonomy that covers what actually arrives wrong, a first automated action for each code, and time-to-resolution measured on four separate clocks rather than one vague one.
The Taxonomy
Ten codes covering essentially everything that goes wrong between the barrier and the goods receipt posting. The point of coding is not tidiness — it is that an uncoded exception cannot trigger an automatic action, cannot be counted, and cannot be attributed to a supplier at the quarterly review.
SHTShortage
DetectedCount at door
OwnerReceiving lead
Fewer units than the despatch advice declares. The most common code and the one most likely to reach the line.
OVROverage
DetectedCount at door
OwnerReceiving lead
More than declared. Harmless in feel, expensive in fact — unplanned stock with no location and no valuation.
WPTWrong part
DetectedScan mismatch
OwnerSupplier quality
Part number does not match the order line. Treat as a nonconformance — segregate, record, then decide refuse or receive to a nonconforming location.
SEQSequence break
DetectedKit verification
OwnerLine feed
Correct parts, wrong order. The plant-specific code that generic receiving processes have no concept of at all.
DMGDamage
DetectedVisual, at door
OwnerReceiving lead
In-transit or handling damage. Evidence has to be captured before the carrier leaves, or the claim is already weak.
LBLLabel fault
DetectedScan failure
OwnerSupplier logistics
Missing, unreadable or non-conforming transport label. Cheap to fix, disproportionately expensive at the door.
ASNAdvice mismatch
DetectedGate or door
OwnerSupplier logistics
Despatch advice missing, unvalidated, or describing something other than what arrived. Blocks every automated step downstream.
QLTQuality reject
DetectedIncoming inspection
OwnerSupplier quality
Characteristic outside specification. Routes into the nonconformance process rather than the logistics one.
PKGPackaging fault
DetectedDoor or line-side
OwnerPackaging engineering
Wrong container, wrong quantity per container, returnables unreconciled. Surfaces at line-side long after receipt.
NSHNo-show
DetectedWindow expiry
OwnerInbound planner
The exception with no trailer. Easily the most under-coded, because nothing physically arrives to prompt anyone.
The uncoded majority
Most plants can produce a discrepancy report and almost none can tell you the split by code, by supplier, by shift. That gap is not administrative — it is why the same supplier sends the same short shipment for eleven consecutive months without anyone noticing a pattern. Analysing past errors for root cause depends entirely on the data existing in the first place.
Five Ways to Cut the Interval
Ordered by effect on time-to-first-action, not by sophistication. The first three need no new system — they need decisions written down before the next exception occurs rather than during it.
01
Detect by scan, not by eye
Scanning every pallet or container against the despatch advice links each unit to the system in real time and flags an unexpected part number or a wrong quantity instantly. Visual verification finds the same problems eventually, but "eventually" is the entire cost. The exception should exist as a record before the person who found it has finished looking at it.
EffectMoves detection from minutes to seconds, and makes the code automatic rather than a judgement
02
Define the first action per code, in advance
Every code needs a defined path decided before anyone is standing at a dock under pressure: accept partial, reject overage, segregate, quarantine, or create an exception record. Damages and shortages are inevitable, so the SOP should carry a simple triage — accept as is within policy, rework, or quarantine and report. What must not happen is that the first action is a phone call to ask what the first action should be.
EffectRemoves the single largest delay component: waiting for a human to decide the obvious
03
Notify by consequence, not by department
A shortage on a sequence-critical part is a line-feed problem before it is a purchasing problem. Route the alert to whoever the exception will hurt first, with the impact already calculated — if a key component is short by five units, planners should know immediately so schedules can be adjusted, not at the end of the shift when the paperwork reaches them.
EffectDownstream recovery starts in parallel with resolution instead of after it
04
Capture evidence at the point of discovery
Photographs, notes and the supplier reference, taken while the trailer is still at the door. Evidence gathered later is weaker, contested more often, and makes claims slower and more emotional than they need to be. For anything routing into nonconformance, the record needs part number, revision, order and lot identification, and the quantities — lot size, inspected, defective — so impact can be assessed rather than estimated.
EffectTurns a monthly argument with the supplier into a settled number
05
Contain in the system, not just physically
Segregating material on the floor is half the job. The stock status has to change too, so the material moves from nettable to non-nettable and cannot be accidentally allocated to another production order while disposition is being decided. Physical segregation without the system status change is how quarantined parts end up on the line anyway.
EffectPrevents the second, worse incident that follows an uncontained first one
The expensive interval is between discovery and first action — and it is almost entirely removable.
A solutions engineer will map your exception codes to first automated actions against your own receiving flow and system landscape, and show where the current path loses time.
First Automated Action, by Code
What the system does the instant the exception is raised, and the narrow condition under which a human is required. Everything a person does before this point is delay, not judgement.
SHTFlag quantity variance, notify line feed with coverage impact, hold goods receipt on the short line onlyHuman if: coverage is breached
OVRCheck against over-receipt tolerance, auto-accept within policy with reason logged, else raise for dispositionHuman if: outside tolerance
WPTBlock receipt, segregate to nonconforming location, open the record, notify supplier quality and purchasingHuman if: always — refuse or receive pending instruction
SEQStop the kit at the cell, flag the affected sequence positions, alert line feed before the container movesHuman if: sort versus stop decision
DMGPrompt photo capture at the door, attach carrier and supplier reference, hold the trailer pending acknowledgementHuman if: accept-as-is judgement
LBLRoute to exception lane rather than the queue, request re-issue, log against supplier logistics scoreHuman if: manual identification needed
ASNDivert at gate, do not admit to staging, notify supplier logistics with the specific validation failureHuman if: sequence-critical load
QLTSet stock non-nettable, quarantine, open the nonconformance with quantities and evidence attachedHuman if: always — disposition required
PKGRecord against the packaging specification, flag returnables variance, notify packaging engineeringHuman if: line-side handling affected
NSHFire on window expiry without arrival, release the reserved door, run coverage check, notify plannerHuman if: coverage exposed
Note how few rows require a human immediately. That is the design intent — three codes always need a person because disposition is a judgement with cost and compliance consequences, and the rest need one only under a stated condition. If your current process requires a human for all ten, the interval you are paying for is mostly waiting, not deciding.
Four Clocks, Not One
"Time to resolution" as a single number is nearly useless, because it averages together four intervals with completely different owners and completely different fixes. Measure them separately and the improvement work becomes obvious.
Clock 1
Occurrence to detection
From the moment the problem existed to the moment somebody or something noticed. Scan-based detection collapses this; visual inspection does not.
Owner: receiving process design
Clock 2
Detection to first action
The interval this whole page is about. Should be near zero for coded exceptions with defined paths. Usually the largest and least visible component.
Owner: exception rules
Clock 3
First action to disposition
Containment done, awaiting a decision — accept, rework, return, scrap. Driven by how fast the right person gets the right information, not by how hard the decision is.
Owner: named approver per code
Clock 4
Disposition to closure
Replacement received, credit raised, corrective action closed. Slowest by far and least urgent — but the clock that shows whether corrective actions ever actually work.
Owner: supplier quality and purchasing
The clock that predicts repeat failures
Clock 4 read alongside repeat occurrence rate is the honest measure of whether a supplier's corrective action solved anything. A supplier who closes corrective actions on schedule and generates the same code again next quarter has a process that produces paperwork rather than change — and that pattern is invisible if you only track a single blended resolution time.
Severity and Response
Not every exception deserves the same urgency, and treating them equally is how genuinely critical ones get diluted. Three tiers, with escalation and target attached. Our analytics and reporting module is where the targets get tracked.
← Swipe to see all columns →
That last row matters more than the three above it. Safety-critical components typically remain on required critical-characteristic verification regardless of how strong a supplier's overall scorecard is, because the consequence of an undetected defect outweighs any efficiency gained from reduced sampling. Encode the override so it cannot be waived by a tier rule.
What the Record Must Contain
Thin exception records are the reason disputes take weeks. This is the minimum for anything routing into nonconformance, and the structure that removes ambiguity from the description itself.
Required fields
Part number, revision level, description
Order and work order reference, lot identification
Lot size, inspected quantity, defective quantity
Supplier identity, for follow-up and scorecard attribution
Carrier and vehicle, where transit damage is possible
Photographs attached at the point of discovery
Detection point, timestamp and detecting method
Assigned code, severity tier and named owner
Write the problem as should-be versus is
Should beDiameter 2.500 ± 0.005 in
IsDiameter 2.515 in
This structure eliminates ambiguity and gives the technical foundation for everything that follows — evaluation, disposition, supplier discussion. Compare it with "parts oversized", which is what most exception records actually say and which supports no decision at all. The same discipline applies to logistics codes: "12 containers declared, 9 received" beats "short delivery" for exactly the same reason.
Metrics Worth Reporting
Six. The first three are usually available already; the last three are the ones that change behaviour.
Exceptions per thousand receipts, by codeThe base rate. Meaningless as a total, informative the moment it is split by code and supplier.
Clock 2 median and 90th percentileDetection to first action. The number that most directly measures whether your rules are working.
Share resolved without human interventionShould rise over time as tolerance policies are encoded. A flat line means the rules were written once and never revisited.
Repeat occurrence rate per supplier per codeFlags suppliers whose corrective actions never solve the underlying problem — the single most useful supplier-quality signal available.
Exceptions escaping to line-sideFound after receipt rather than at the door. Every one is a detection failure, and packaging faults dominate this list.
Cost of managing the exceptionReplacement parts, miscellaneous charges and the timesheet hours to correct it. Rarely captured, and the only figure that makes prevention fundable.
Map Your Codes to First Automated Actions
Bring your current discrepancy categories, your receiving flow and your system landscape. A solutions engineer maps them onto the taxonomy, defines the first automated action per code against your own tolerance policies, and sets out the four clocks with what each one needs to be captured. Works alongside your existing quality process rather than replacing it.
Coded exception taxonomy
Automated first action
Four-clock TTR measurement
Evidence capture at the door
Frequently Asked Questions
How granular should the taxonomy be?
Granular enough that every code maps to a distinct first action, and no more. Ten to fifteen codes covers a plant comfortably. The test is simple: if two codes would trigger identical automated behaviour and identical ownership, merge them. If one code would trigger different behaviour depending on circumstances, split it. Taxonomies fail in both directions — too coarse and nothing can be automated, too fine and nobody selects the right code under pressure at a dock face.
Should a wrong part be refused at the dock or received?
Decide it as a policy rather than at the door. The standard treatment is to handle it as a nonconformance — segregate it, record the details, and then decide whether to refuse at the dock or receive it into a nonconforming location pending supplier instruction. Which of those two is right depends on your return logistics and whether the supplier can instruct quickly. What matters is that the segregation and the record happen automatically first, so the decision can be taken calmly rather than while a driver waits.
Why is physical quarantine not enough on its own?
Because the system will keep offering the material to production. The stock status has to change alongside the physical move so the material becomes non-nettable and cannot be allocated to another production order while disposition is being determined. Sites that segregate physically but not systemically eventually consume quarantined parts anyway — usually during a shortage, when someone finds stock the system says is available. The dual approach is what makes containment real.
Who should be notified first on a shortage?
Whoever the shortage will hurt first, which on a sequence-critical part is line feed rather than purchasing. Notify by consequence, not by department. If a key component is short by five units, planners need to know immediately so schedules can be adjusted — and the notification should carry the coverage impact already calculated rather than leaving the recipient to work out whether it matters. Purchasing and supplier quality still get notified; they just are not the ones who need to act in the next ten minutes.
Does incoming inspection catch quality exceptions reliably?
Only partially, and it is worth being honest about the limit. A supplier can pass incoming inspection for months and still be one tooling change away from a serious problem, because the sample never happened to catch the drift. A larger sample catches more of what is already wrong in the current lot but says nothing about the next one. Visibility into the supplier's own process data is what flags problems before they generate a nonconformance at receiving. Treat inspection as a net, not a guarantee.
How do we stop the same exception recurring?
Track repeat occurrence per supplier per code, and read it alongside corrective action closure time. A supplier closing actions on schedule while generating the same code again is producing paperwork rather than change, and that is only visible when exceptions are coded and attributed. Then use the pattern rather than the incident in supplier reviews — eleven identical shortages over a year is a conversation that goes somewhere, while the eleventh shortage on its own is one more incident to explain away.
What is realistic to automate in the first phase?
Detection, coding, notification and containment. Disposition mostly stays human, and should — accept, rework, return or scrap carries cost and compliance weight that belongs with a named owner. The gain in phase one comes almost entirely from collapsing clock 2, which is usually the largest interval and the one nobody measures. Once that is in place, encoding tolerance policies lets a share of low-severity codes resolve without intervention at all. Our
integrations overview covers the system handoffs required.
Make the First Action Automatic
A coded taxonomy that covers what actually arrives wrong, a defined first action for every code, containment in the system as well as on the floor, and four clocks that show exactly where the time goes.
Works alongside existing QMS · Runs on existing handsets · Site-level configuration