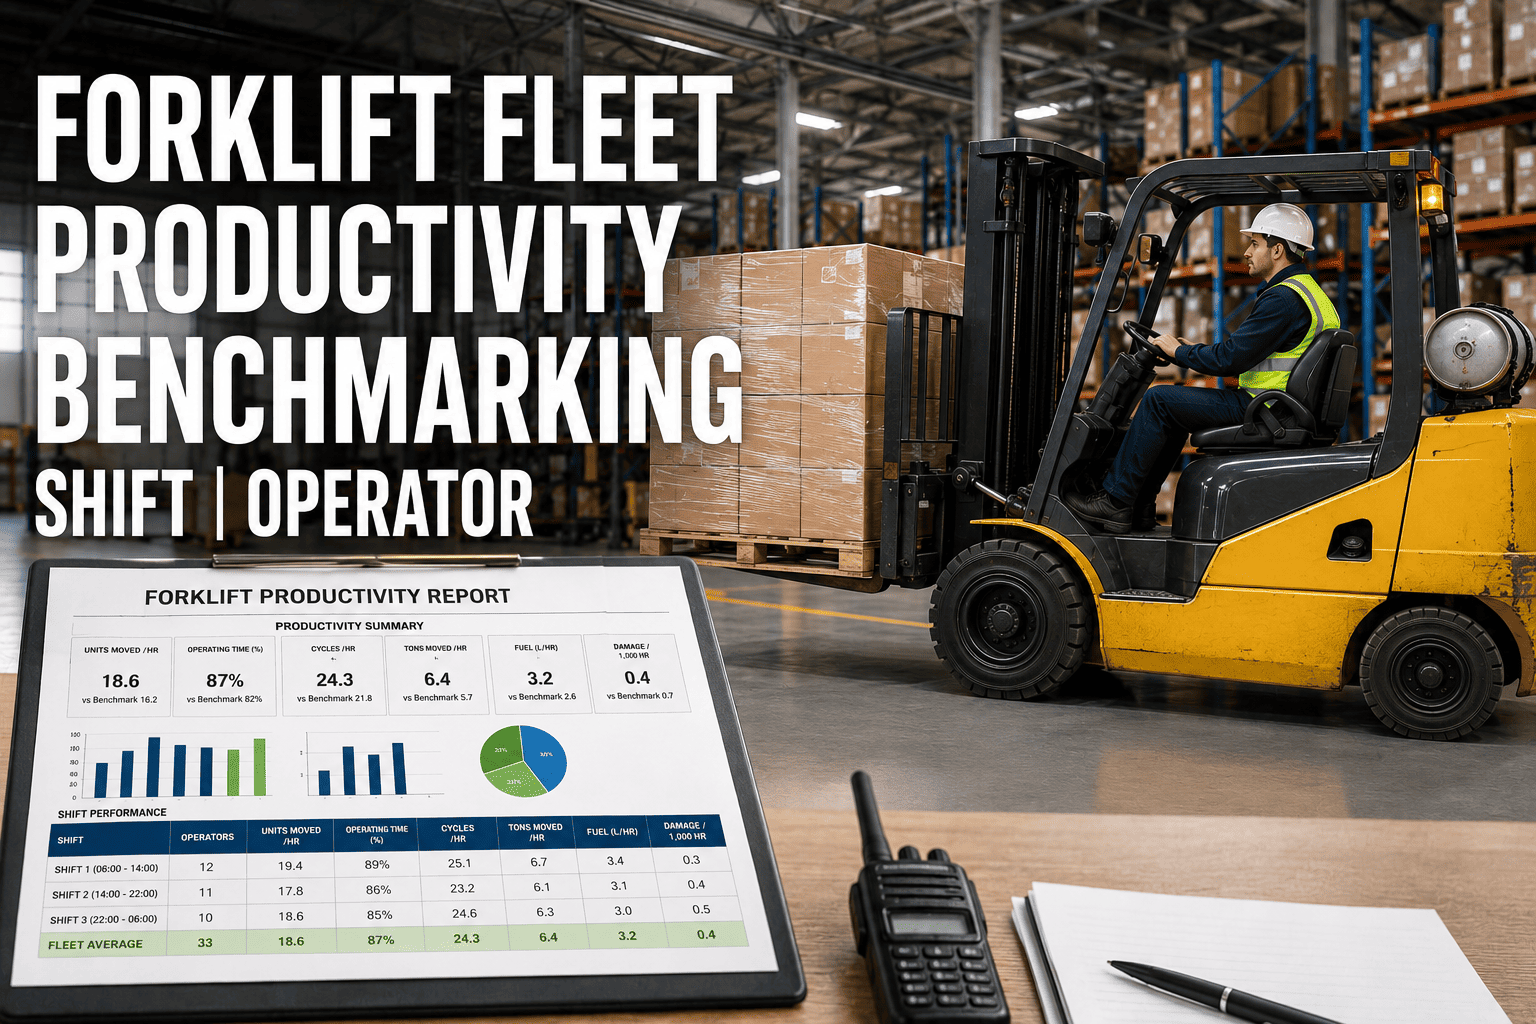
Material handling accounts for 15 to 40 percent of total operating costs in manufacturing plants, yet most facilities have no reliable way to measure how efficiently their forklifts, tuggers, and pallet jacks are actually working. Plant managers can tell you exactly how many units they produced last shift, but ask about forklift utilization rates or average move cycle times and the room goes quiet. This blind spot costs manufacturing operations hundreds of thousands of dollars annually in hidden waste. The problem is not that plants do not care about efficiency. The problem is that material handling has always been treated as a support function rather than a measurable process, leaving enormous improvement potential completely invisible.
Material handling consumes 15 to 40 percent of plant operating costs but most facilities measure less than 10 percent of handling activity. Forklift utilization typically ranges from 30 to 55 percent meaning nearly half of every shift is non-productive. Plants that implement systematic measurement reduce handling costs by 20 to 35 percent within the first year through better utilization, reduced deadhead travel, and optimized fleet sizing.
Why Material Handling Efficiency Stays Unmeasured
Manufacturing plants excel at measuring production output because it directly connects to revenue. Units produced, cycle times, scrap rates, and overall equipment effectiveness get tracked meticulously on every production line. Material handling exists in the spaces between those production lines, moving raw materials to stations and finished goods to shipping docks. Because handling does not transform the product, it gets categorized as overhead rather than a value-adding process worth measuring. This mindset creates a massive data gap. Plant managers know their production line runs at 85 percent OEE but have no equivalent metric for the forklift fleet that feeds that line. When a production line stops because material did not arrive on time, the root cause gets logged as a production delay rather than a handling failure, further masking the real problem.
The second reason measurement lags is technical limitation. Traditional approaches rely on periodic observation studies where someone stands with a clipboard watching forklifts for a few hours and extrapolating findings. These studies are expensive, suffer from observer bias, and capture only a snapshot rather than continuous reality. A forklift operator behaves differently when being watched. The data from a two-day observation study cannot represent the variation that occurs across weeks, shifts, and seasonal demand changes. Without automated measurement tools, plants are forced to either accept incomplete data or abandon measurement entirely. Sign up for FleetRabbit to replace manual observation with continuous automated measurement that captures every move, every idle minute, and every route across all shifts.
The Five Core Metrics That Reveal Handling Efficiency
Measuring material handling efficiency requires tracking specific metrics that expose where time, money, and capacity are being wasted. These five metrics provide a complete picture of handling performance when measured continuously rather than through periodic samples.
Forklift Utilization Rate
Utilization rate measures the percentage of shift time a forklift spends performing productive work versus sitting idle, waiting for tasks, or traveling empty. True utilization separates productive lift-and-carry time from all other activities. A forklift moving a pallet from receiving to production is productive. A forklift driving empty from production back to receiving is deadhead travel, not productive utilization. Most plants discover their true utilization rate is 15 to 20 percent lower than assumed because idle and waiting time goes uncounted in manual tracking. Measuring utilization accurately reveals whether you have too many or too few vehicles. Plants typically find they can reduce fleet size by 15 to 30 percent without any impact on service levels once utilization data guides right-sizing decisions.
Deadhead Travel Percentage
Deadhead travel occurs whenever a forklift moves without carrying a load. Every empty trip represents wasted time, wasted energy, and unnecessary equipment wear. Deadhead percentage is calculated by dividing empty travel distance or time by total travel distance or time. A deadhead percentage of 40 percent means nearly half of all forklift travel produces no value. High deadhead percentages indicate poor route planning, imbalanced material flows, or staging locations that create excessive return trips. Reducing deadhead from 45 percent to 30 percent through better staging and route optimization can cut total travel time by 20 percent, directly increasing productive capacity without adding equipment.
What Drives High Deadhead Percentages
Several structural factors push deadhead percentages above optimal levels. Point-to-point material flows where forklifts pick up at one fixed location and deliver to another fixed location naturally create 50 percent deadhead because every loaded trip requires an empty return. Zone-based staging where materials are pre-positioned near consumption points reduces deadhead by shortening empty return distances. Imbalanced workflows where one area generates more outbound material than inbound material creates directional empty travel. Understanding these patterns requires route-level data that shows exactly where empty travel occurs, not just aggregate percentages.
Move Cycle Time
Move cycle time measures the total duration from when a forklift receives a task assignment to when the material is placed at the destination. This includes travel time to pickup, load time, travel time to destination, and unload time. Cycle time varies by move type, distance, and load characteristics. Tracking cycle times by route and move type reveals which handling paths are efficient and which have excessive variability. High variability in cycle times for the same route indicates inconsistent processes, congestion, or operator-dependent performance differences. Standardizing cycle times reduces variability and enables reliable production scheduling because material arrival becomes predictable rather than estimated.
Tasks Completed Per Shift
Tasks completed per shift provides the most direct measure of handling productivity. This metric counts the number of discrete material moves each forklift completes during a shift. Comparing tasks per shift across operators, shifts, and vehicles immediately highlights performance differences. A forklift completing 45 tasks per shift on day shift while the same route averages 32 tasks on night shift reveals a training, staffing, or workflow problem. Tracking this metric over time shows whether efficiency improvements are actually delivering more throughput or just shifting the same work around differently. Plants that begin measuring tasks per shift typically discover a 20 to 40 percent performance gap between their best and worst operators on identical routes.
Cost Per Material Move
Cost per move calculates the total expense of executing a single material handling task including operator labor, equipment depreciation, maintenance allocation, and energy consumption. This metric translates operational data into financial terms that resonate with leadership. When a plant manager can show that the average material move costs 14 dollars and 25 percent of moves are unnecessary, the math becomes compelling. Eliminating unnecessary moves saves real dollars that flow directly to the bottom line. Cost per move also enables meaningful comparisons between handling methods. If a tugger train move costs 6 dollars while a forklift move for the same route costs 14 dollars, the investment case for tugger trains becomes quantifiable rather than anecdotal.
FleetRabbit tracks utilization, deadhead travel, cycle times, tasks per shift, and cost per move automatically across your entire forklift fleet. No clipboards, no observation studies, no guesswork. See exactly how your handling operation performs on every shift, every day. Start measuring with a free trial.
How to Calculate Each Metric Accurately
Accurate calculation requires continuous automated data collection rather than periodic sampling. Manual observation captures perhaps 2 to 5 percent of total handling activity, creating massive sampling error. Automated measurement through telematics captures 100 percent of activity across all shifts, all vehicles, and all days. The calculation methodology differs for each metric but all depend on the same underlying data foundation of continuous position and status tracking.
| Metric | Calculation Formula | Data Required | Benchmark Range |
|---|---|---|---|
| Forklift Utilization | Productive time divided by total shift time multiplied by 100 | Lift activity, travel with load, shift start and end times | 50 to 70 percent is good, below 40 percent indicates over-fleeting |
| Deadhead Percentage | Empty travel distance divided by total travel distance multiplied by 100 | GPS position data, load status sensor, travel distance logs | 25 to 35 percent is achievable, above 45 percent needs optimization |
| Move Cycle Time | Task completion timestamp minus task assignment timestamp | Task assignment logs, destination arrival timestamps, load placement confirmation | Varies by route, target is less than 15 percent standard deviation |
| Tasks Per Shift | Total completed moves divided by number of shifts operated | Move completion logs, operator assignment records, shift schedules | Route dependent, target less than 20 percent gap between best and worst |
| Cost Per Move | Total handling costs divided by total moves completed in period | Labor costs, depreciation schedules, maintenance records, energy costs, move counts | 8 to 15 dollars for standard moves, above 20 dollars signals inefficiency |
Common Measurement Mistakes to Avoid
Relying on Operator Self-Reporting
Asking forklift operators to log their own activities creates systematically inaccurate data. Operators estimate time spent on different activities from memory at the end of a shift, and human estimation consistently underreports idle time while overreporting productive time. Studies comparing self-reported activity logs against automated telematics data show self-reporting overstates productive utilization by 15 to 25 percent. This inflation makes handling appear more efficient than it actually is, preventing accurate problem identification and hiding improvement opportunities.
Measuring Averages Instead of Distributions
Reporting average utilization or average cycle time hides the variability that matters most. An average cycle time of 8 minutes looks acceptable until you examine the distribution and discover that 30 percent of moves take 12 to 18 minutes while 20 percent take 3 to 5 minutes. That variability is what disrupts production scheduling because predictable material flow requires consistent cycle times, not just acceptable averages. Measuring distributions through percentile tracking, standard deviations, and frequency histograms reveals the real operational picture that averages obscure.
Ignoring Shift-to-Shift Variation
Many plants measure handling efficiency on a single shift and assume findings apply across all shifts. In reality, handling efficiency often varies dramatically between day, swing, and night shifts due to different staffing levels, production schedules, supervisor attention, and operator experience. A plant measuring 55 percent utilization on day shift might discover night shift operates at only 35 percent because reduced supervision allows more idle time and less efficient routing. Aggregating data across shifts without separating shift-level performance hides these differences and prevents targeted improvement.
Not Connecting Handling Metrics to Production Impact
Measuring handling efficiency in isolation misses the most powerful insight available. The ultimate purpose of material handling is to keep production lines fed with materials and finished goods moving to shipping. When handling metrics are connected to production data, you can directly measure how handling delays cause production stoppages, how handling speed improvements increase line throughput, and how handling reliability improvements reduce safety stock requirements. This connection transforms handling measurement from an interesting operations exercise into a strategic profitability tool. Book a demo to see how FleetRabbit connects handling data with production outcomes.
FleetRabbit installs in under an hour and begins capturing real utilization, travel, and task data immediately. Within the first week you will see exactly where your forklift fleet wastes time and money. Within the first month you will have the data to make fleet-right-sizing and route optimization decisions with confidence.
From Measurement to Action: Building an Improvement Cycle
Measuring material handling efficiency creates value only when the data drives specific operational changes. The most effective plants establish a continuous improvement cycle that turns measurement into action within days rather than months. The cycle begins with baseline measurement. Deploy automated tracking across all forklifts and material handling equipment for two to four weeks without making any changes. This baseline captures normal operating patterns across all shifts and all days of the week. The baseline data often reveals surprises. Plants frequently discover that their assumed highest-traffic routes are not actually the busiest, that their newest forklifts have the lowest utilization, or that their most experienced operators have the highest deadhead percentages because they have developed inefficient habits over years without feedback.
Identify the Highest-Impact Improvement Opportunities
Not all efficiency improvements deliver equal value. Prioritize opportunities by multiplying the improvement potential by the financial impact. A 10 percent utilization improvement on a high-use forklift operating two shifts daily delivers far more value than a 25 percent improvement on a low-use vehicle operating one shift. Focus initial efforts on the 20 percent of vehicles and routes that represent 80 percent of handling activity. This concentration of effort delivers visible results quickly, building organizational support for broader changes. Common high-impact opportunities include right-sizing the fleet by removing underutilized vehicles, consolidating overlapping routes that send multiple forklifts to the same area, and rebalancing staging locations to reduce deadhead travel on high-frequency routes.
Implement Changes in Controlled Phases
Implement one to three changes at a time rather than attempting a complete handling overhaul. Changing too many variables simultaneously makes it impossible to determine which changes delivered results and which had no effect. Each phase should last two to four weeks, providing enough data to measure the impact of changes against the baseline. If removing two forklifts from a specific zone reduces utilization on remaining vehicles from 45 percent to 62 percent without increasing cycle times, the right-sizing decision is validated. If cycle times increase significantly, the vehicles can be returned and a different approach attempted. This phased method controls risk while building a evidence-based improvement track record.
Establish Ongoing Performance Monitoring
Once improvements are implemented, continuous monitoring ensures gains are sustained rather than eroding over time. Handling efficiency naturally degrades as operators develop workarounds, staging locations drift from optimal positions, and new products or routes are added without being measured. Weekly performance dashboards showing the five core metrics against targets keep handling efficiency visible to operations leadership. Monthly reviews comparing current performance to baseline quantify the financial impact of improvements and identify emerging problems before they become serious. Plants that maintain continuous monitoring sustain 85 to 90 percent of initial efficiency gains over time, while plants that measure once and stop typically lose 40 to 60 percent of gains within six months as old habits return.
What Good Looks Like: Efficiency Benchmarks by Plant Type
Benchmarks vary by manufacturing type because material handling complexity differs significantly across industries. High-volume repetitive manufacturing with fixed material flows achieves higher utilization rates because routes are predictable and standardized. Custom or batch manufacturing with variable material flows naturally shows lower utilization and higher cycle time variability. Understanding benchmarks for your specific plant type prevents unrealistic expectations and focuses improvement efforts on achievable targets.
| Plant Type | Utilization Target | Deadhead Target | Cost Per Move Target |
|---|---|---|---|
| High-Volume Assembly | 60 to 72 percent | 22 to 30 percent | 6 to 10 dollars |
| Batch Manufacturing | 48 to 60 percent | 30 to 40 percent | 10 to 16 dollars |
| Process Manufacturing | 42 to 55 percent | 35 to 45 percent | 12 to 20 dollars |
| Warehouse-Connected Plant | 55 to 68 percent | 25 to 35 percent | 8 to 14 dollars |
| Heavy Manufacturing | 38 to 52 percent | 35 to 48 percent | 15 to 25 dollars |
The Financial Impact of Measuring Material Handling Efficiency
The financial return from measuring and improving material handling efficiency is substantial and typically arrives faster than most other operational improvement initiatives. Consider a mid-size manufacturing plant operating 25 forklifts across two shifts. If average utilization is 42 percent and benchmark data shows 58 percent is achievable, the gap represents significant hidden capacity. Bringing utilization from 42 percent to 58 percent through better dispatching, route optimization, and fleet right-sizing typically allows removal of 4 to 6 vehicles. Each forklift costs 35000 to 55000 dollars annually in depreciation, maintenance, energy, and insurance. Removing 5 vehicles saves 175000 to 275000 dollars per year in direct equipment costs. Additional savings come from reduced operator labor for eliminated vehicles, lower energy consumption, and reduced maintenance facility burden.
Deadhead reduction delivers parallel savings. If a 25-forklift fleet drives an average of 180 miles per shift with 42 percent deadhead, reducing deadhead to 28 percent eliminates approximately 7 miles of empty travel per forklift per shift. Across 25 forklifts and two shifts daily, that is 350 miles of eliminated empty travel per day. At an estimated operating cost of 1.50 to 2.50 dollars per mile including fuel, tire wear, and maintenance, deadhead reduction saves 525 to 875 dollars daily or 135000 to 225000 dollars annually. Combined with fleet right-sizing savings, total annual improvement often exceeds 300000 dollars for a plant of this size, delivered primarily through better data visibility rather than capital investment. Sign up for FleetRabbit today to start capturing these savings in your plant.
Material handling waste is invisible only because you are not measuring it. FleetRabbit makes every idle minute, every empty mile, and every unnecessary move visible and actionable. Plants using FleetRabbit reduce handling costs by 20 to 35 percent within the first year through data-driven fleet right-sizing, route optimization, and utilization improvement. Start your free trial today and see your real numbers within a week.